English
- English
- Español
- Português
- русский
- Français
- 日本語
- Deutsch
- tiếng Việt
- Italiano
- Nederlands
- ภาษาไทย
- Polski
- 한국어
- Svenska
- magyar
- Malay
- বাংলা ভাষার
- Dansk
- Suomi
- हिन्दी
- Pilipino
- Türkçe
- Gaeilge
- العربية
- Indonesia
- Norsk
- تمل
- český
- ελληνικά
- український
- Javanese
- فارسی
- தமிழ்
- తెలుగు
- नेपाली
- Burmese
- български
- ລາວ
- Latine
- Қазақша
- Euskal
- Azərbaycan
- Slovenský jazyk
- Македонски
- Lietuvos
- Eesti Keel
- Română
- Slovenski
- मराठी
- Srpski језик
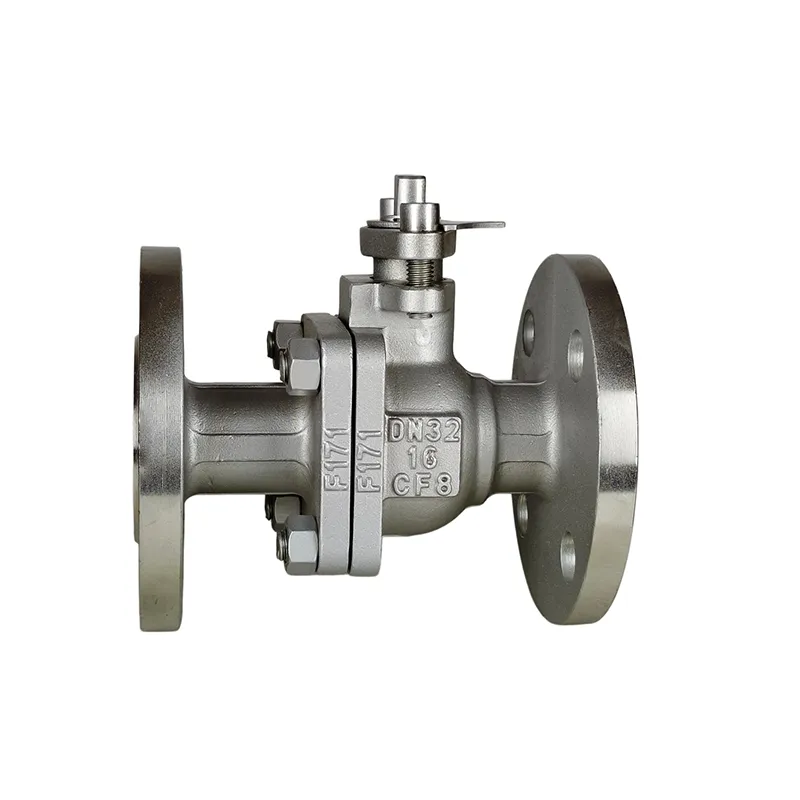
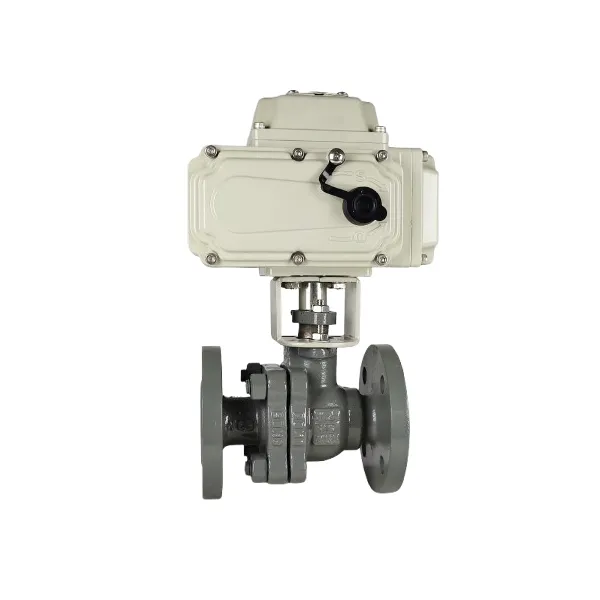
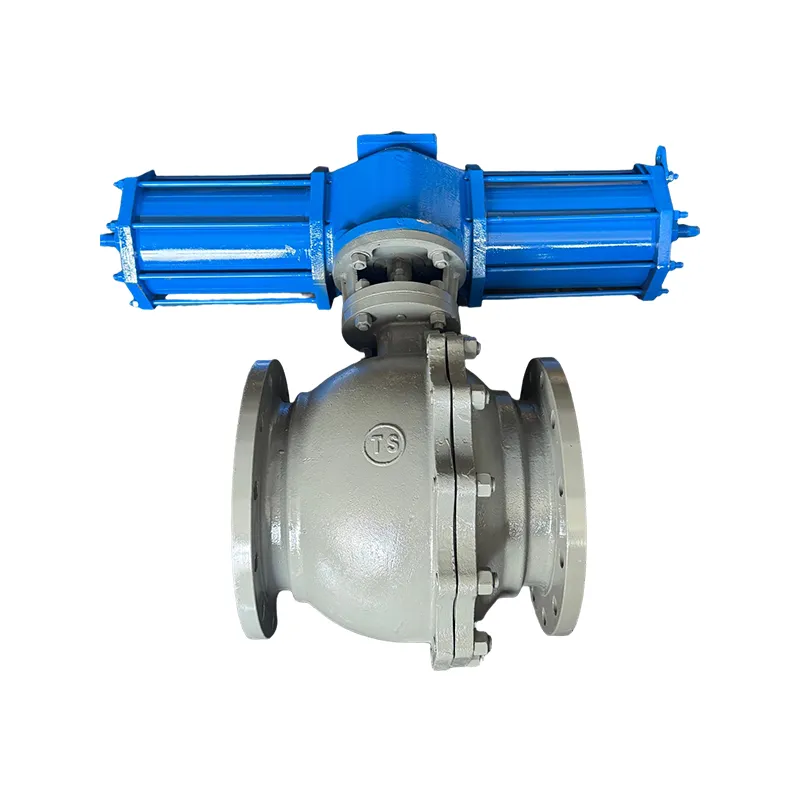
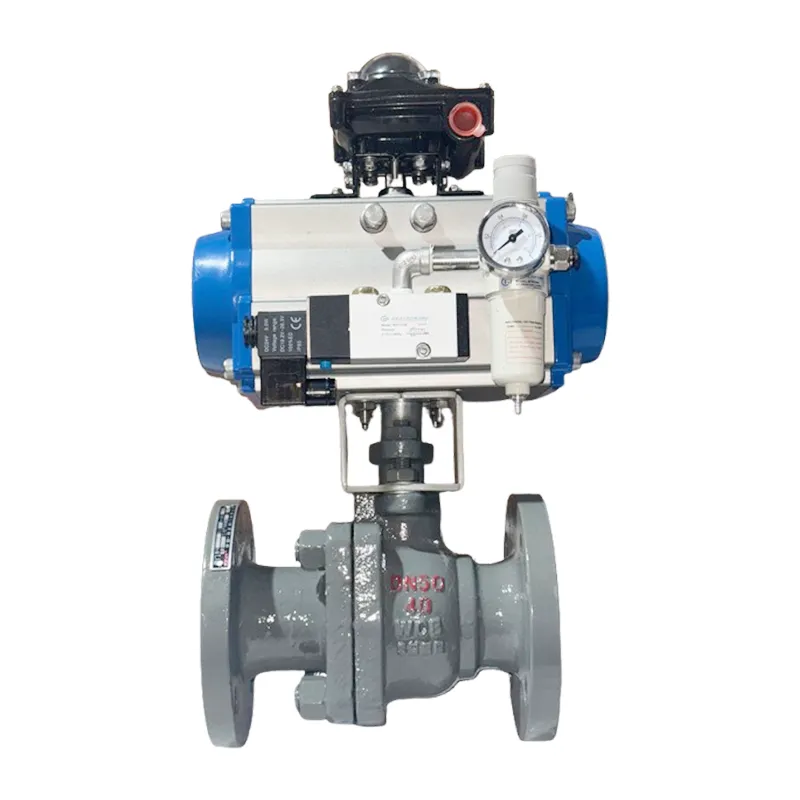
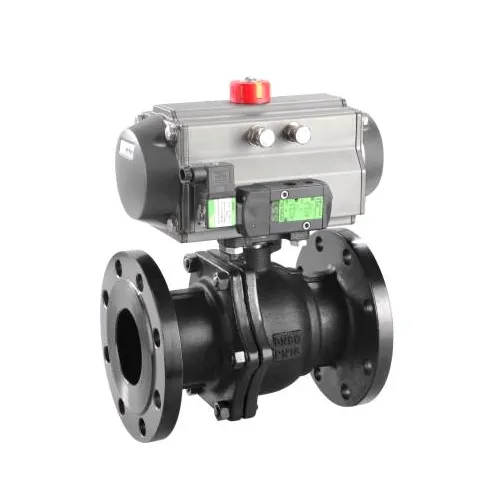
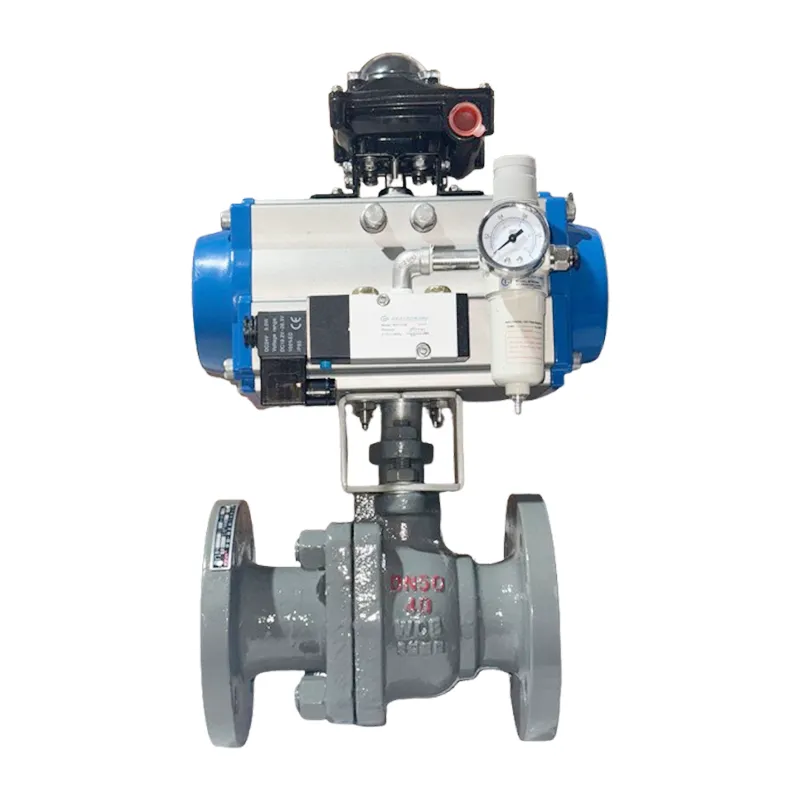
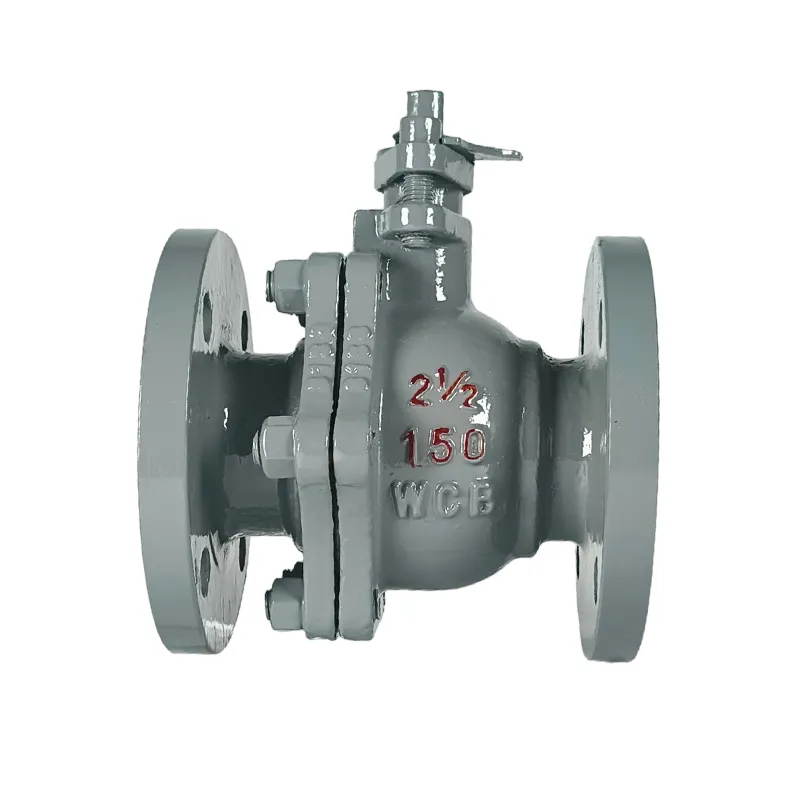
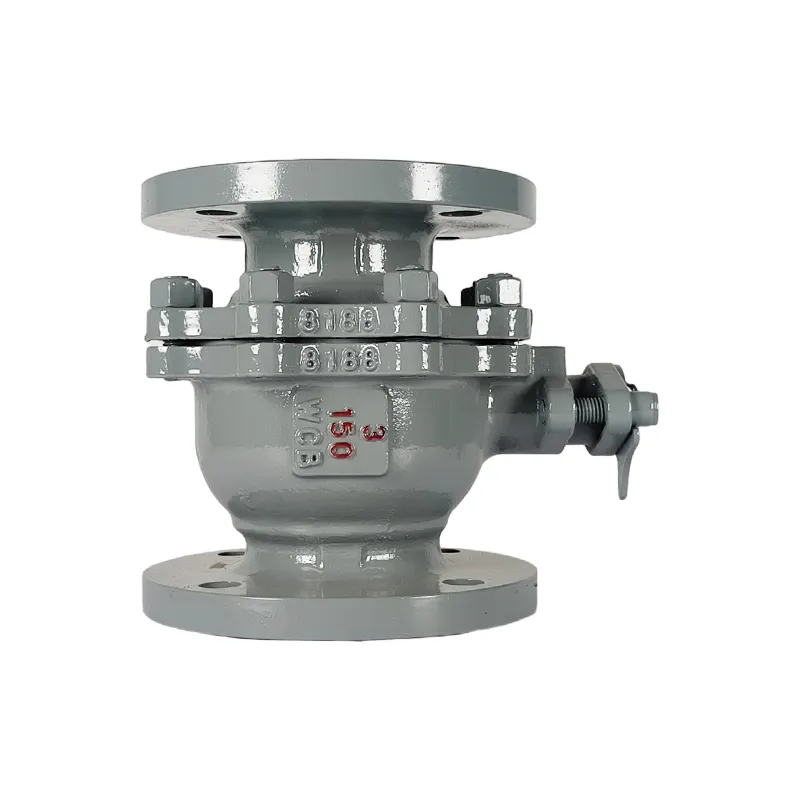
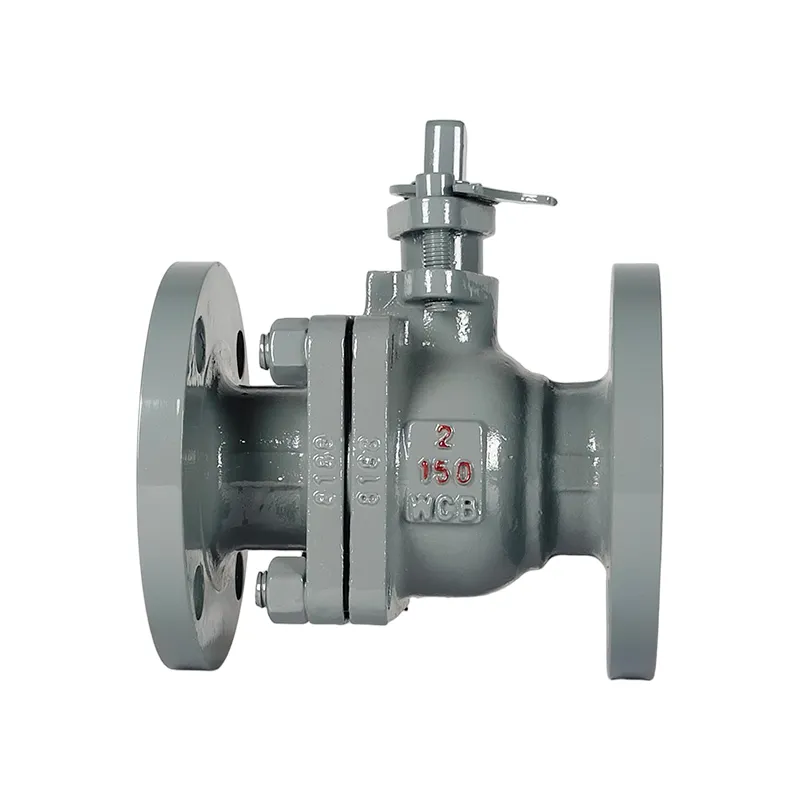
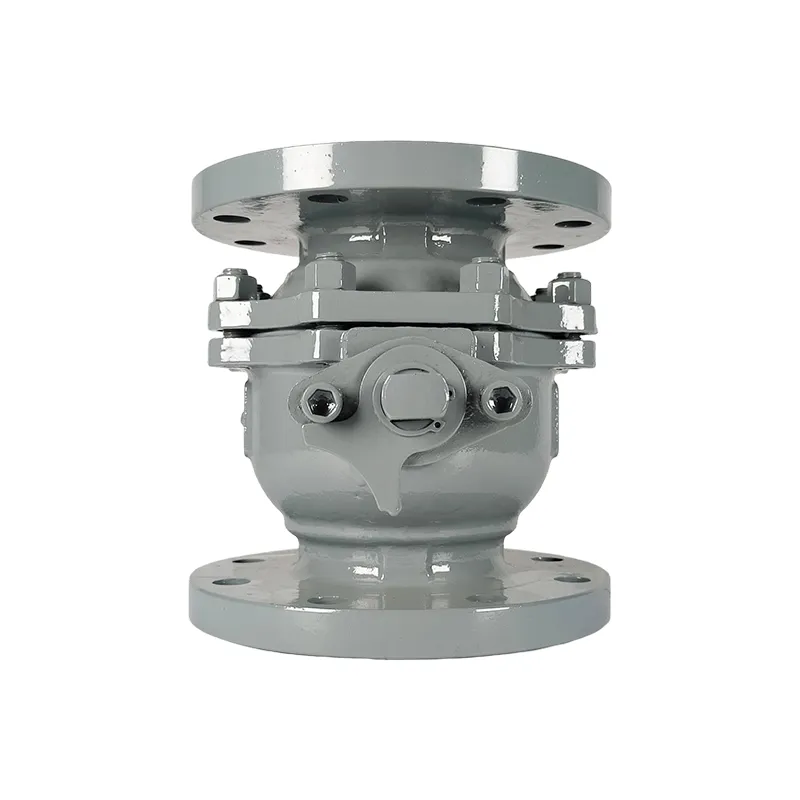
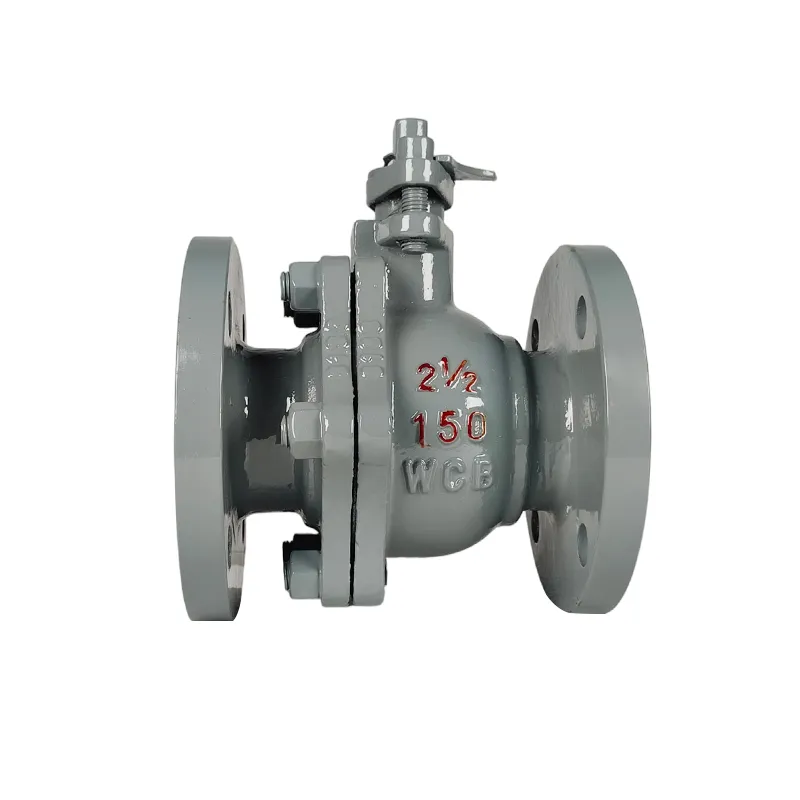
Pneumatic Actuated Flanged Ball Valve
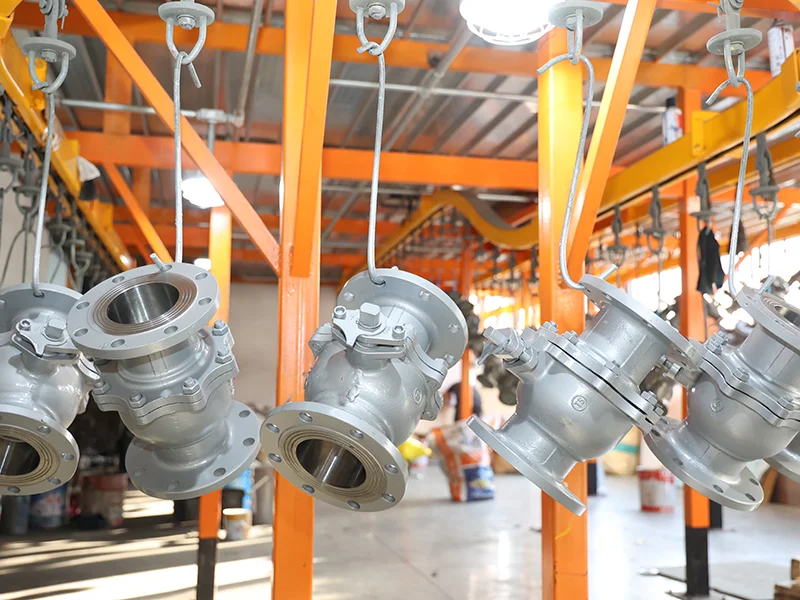
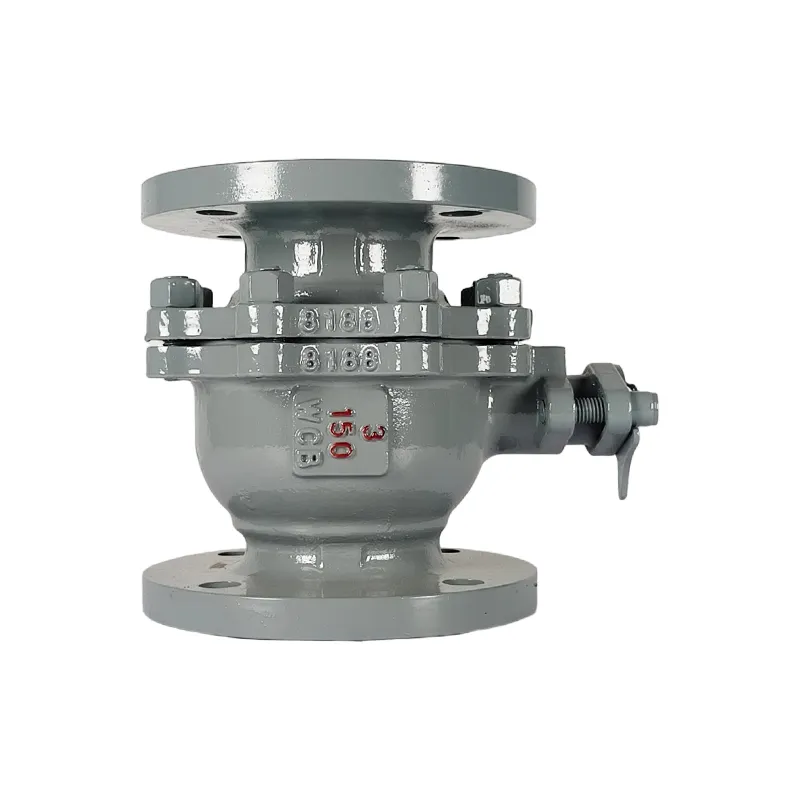
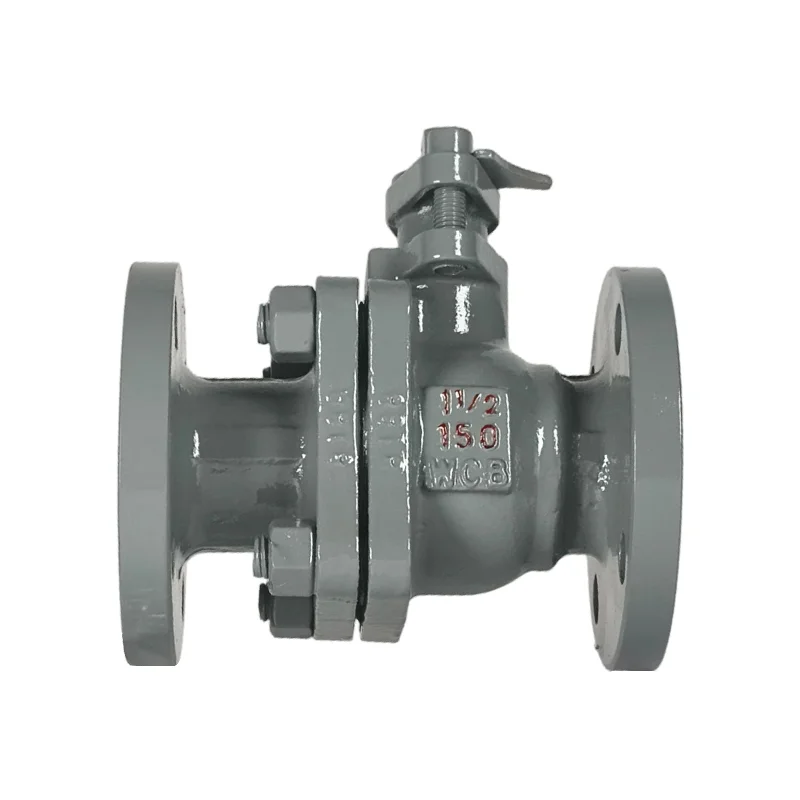
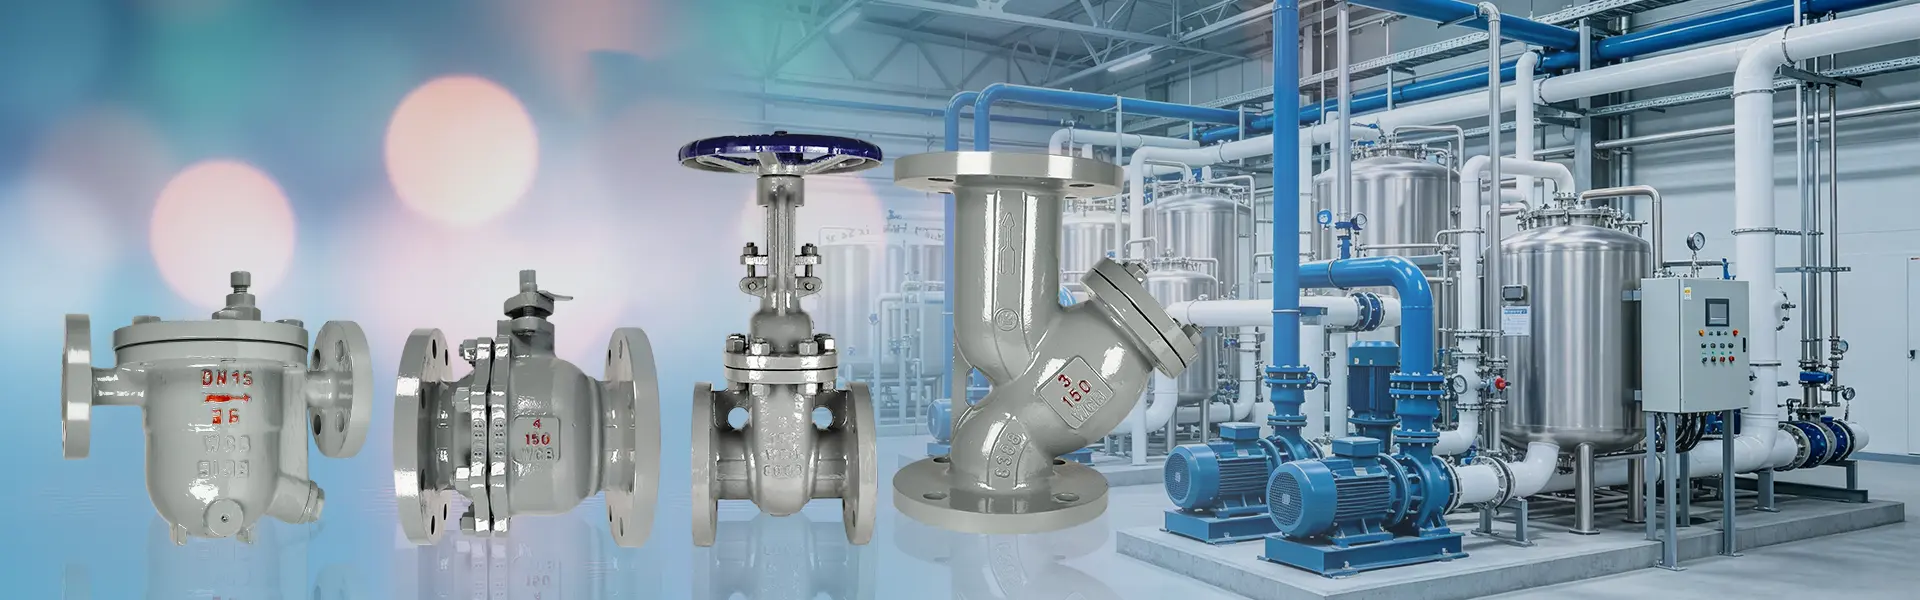
Pneumatic Actuated Flanged Ball Valve from Xiangzheng factory is built with WCB, 304 and 316L stainless steel bodies, precision CNC machining and pneumatic actuators for automated pipeline operation. We follow a complete quality management system and provide OEM/ODM custom solutions. Please feel free to enquire!
Pneumatic Actuated Flanged Ball Valves are engineered for robust industrial piping systems, featuring a sturdy cast body, precision-machined ball and reliable seat sealing for long-term tight shut-off. The matched pneumatic actuator enables quick 90-degree quarter-turn operation, supporting fail-safe modes to meet process safety demands, and allows seamless integration with automated control systems for remote adjustment and emergency isolation. Flanged end connections simplify installation and maintenance, while optional soft and hard seal variants adapt to different temperatures, pressures and media conditions. These valves deliver low flow resistance and consistent performance, widely used across oil & gas, power, chemical and general industrial piping for daily automated flow control and pipeline safety management.
Application Scenarios
● Petrochemical industry: Oil pipelines, refineries, chemical process lines, for flow control and emergency shut-off
● Power & thermal systems: Steam, hot water and fuel pipelines, boiler and heating system control
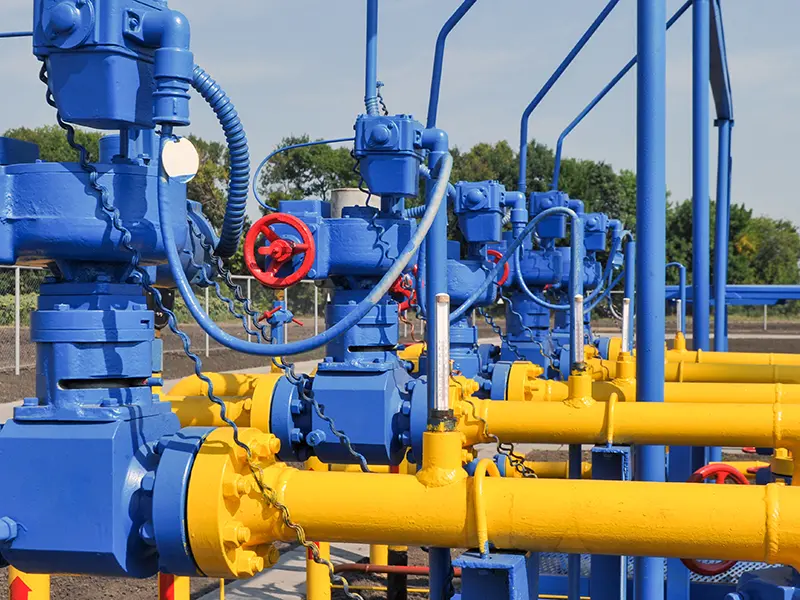
● Municipal gas pipelines: Natural gas transmission networks, pressure regulation and safety cut-off
● Water treatment & environmental projects: Water supply, wastewater treatment and flue gas treatment lines
● HVAC & district heating: Central air conditioning, circulating water and heating pipe networks
● Metallurgy, paper, food & pharmaceutical industries: Production process pipeline control
● Tank farms & terminals: Oil/chemical storage and loading pipelines, remote safety isolation
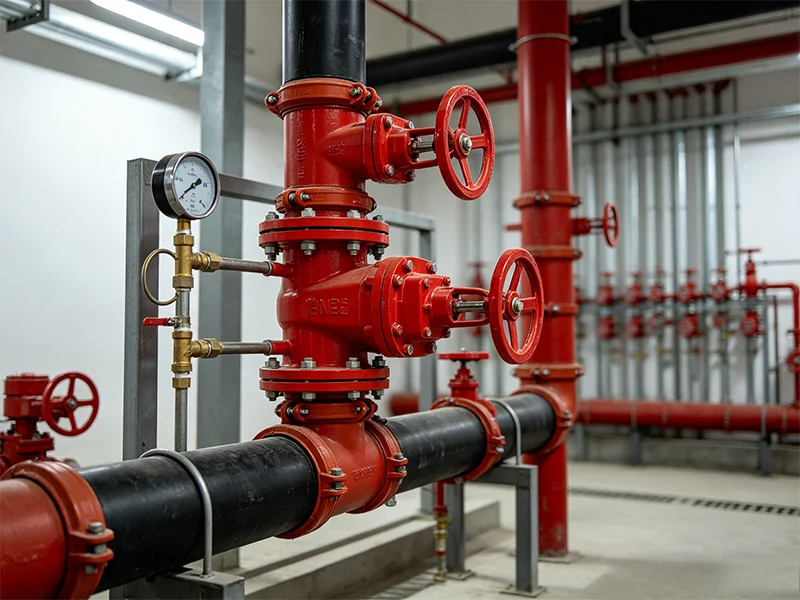
These valves suit automated pipelines requiring remote control, fast switching and emergency shut-off.
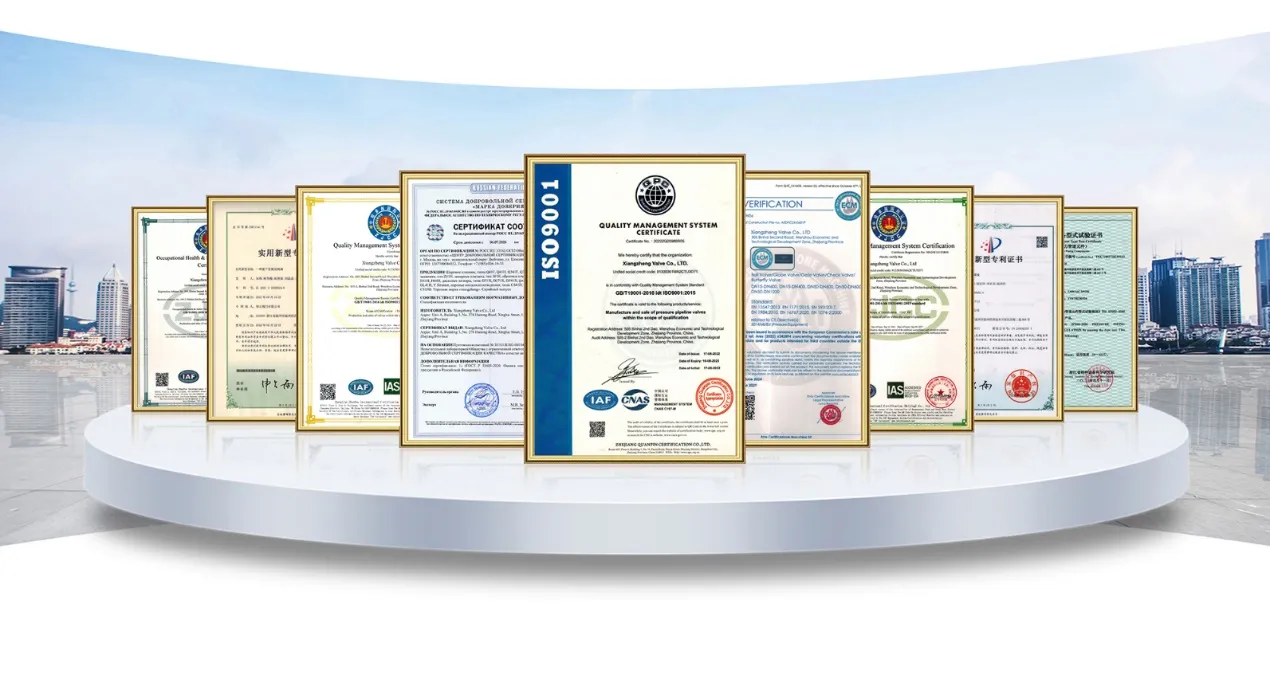
Certifications & Patent
Xiangzheng places strong emphasis on product quality management, manufacturing standards, and continuous technology improvement. The company has established a complete quality control system covering raw material inspection, machining, assembly, pressure testing, sealing testing, surface treatment, and final inspection.
Our company has obtained ISO9001 Quality Management System Certification, ISO14001 Environmental Management System Certification, ISO45001 Occupational Health and Safety Management System Certification, CE Certification, EAC Certification, and GOST Certification, ensuring that our industrial valves meet the requirements of different international markets.
With continuous investment in valve technology development, Xiangzheng Valve has obtained 7 independent patent certificates, including innovations related to valve structure optimization and flow control performance improvement. These technical achievements support our ability to provide customized valve solutions for oil & gas, chemical, power, water treatment, and other industrial applications.
Send Inquiry
Contact Info
-
Address
Workshop 101, Building 3, No. 278 Haitong Road, Xinghai Street, Longwan District, Wenzhou City, Zhejiang Province, China
-
Tel
-
Email
we enhance our competitiveness by exploring new markets and developing new products. We always keep in mind the needs of our customers and the expectations of our end users to optimize our product design and services.
News Recommendations